09. 16, 2026
A CNC Pipe Threading Lathe Machine for Oil and Gas Industry Applications is a large-bore oil-country lathe designed to machine accurate internal and external threads on casing, tubing, drill pipe, couplings, and other long cylindrical components. Its main advantages come from a large spindle bore, rigid bed construction, synchronized CNC threading, and support arrangements for heavy workpieces. I use these four factors as the starting point when evaluating machines for OCTG and oilfield pipe production.
!
A CNC pipe threading lathe is a computer-controlled turning machine built around long, hollow, and often heavy cylindrical workpieces. Unlike a general-purpose CNC turning center, it normally provides a much larger spindle bore, stronger chucking arrangements, longer machining capacity, and thread-cutting cycles designed for pipe ends. In oil and gas manufacturing, it is used for casing, tubing, drill pipe, couplings, pup joints, subs, and selected pipeline components.
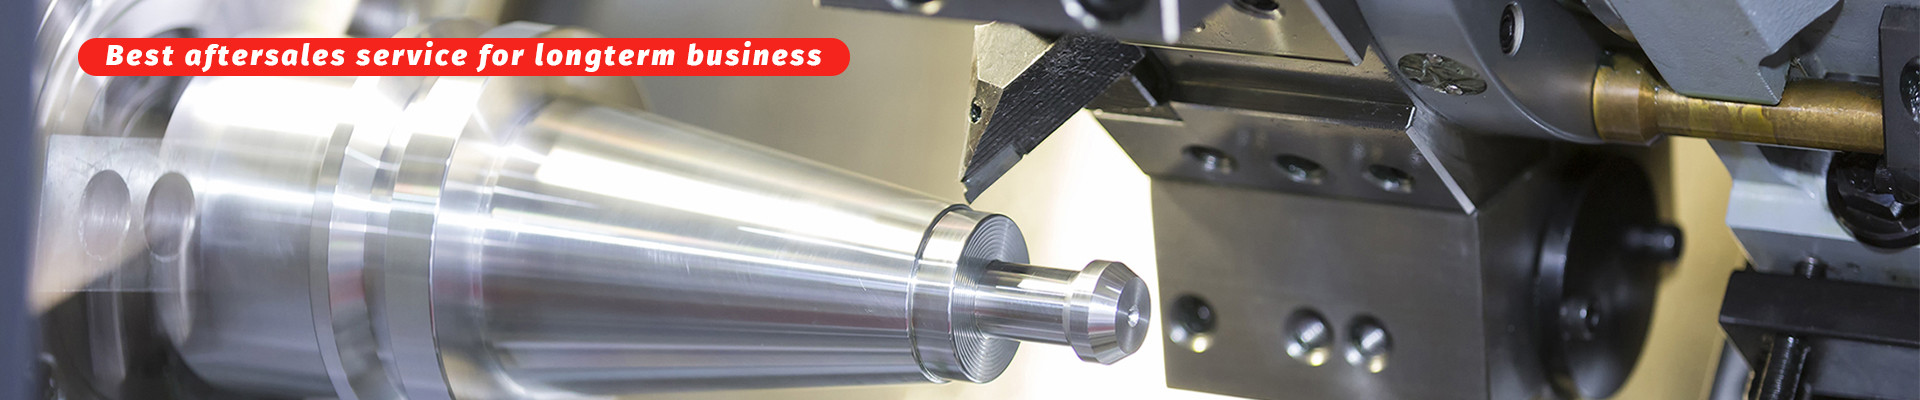
The machine removes material from a pipe end to create an external or internal thread profile. It can also perform facing, chamfering, boring, grooving, taper turning, and thread relief operations in the same setup. Depending on the control, tooling, and machine configuration, the lathe may support metric, inch, taper, NPT, BSP, and API-related thread machining.
The phrase CNC oil country lathe machine generally refers to a CNC pipe lathe designed for oil-country tubular goods, commonly called OCTG. I do not treat the name alone as proof of suitability; I verify the spindle bore, maximum diameter, workpiece length, chuck type, motor torque, thread-pitch range, inspection method, and documented acceptance results.
The most common application is end machining for casing and tubing. These pipes require controlled thread geometry, accurate pitch, suitable taper, and a reliable sealing or connection arrangement. The machine must also maintain alignment when the workpiece is long, thin-walled, or difficult to support without deformation.
Drill pipe production creates a different demand because the workpiece may combine long tubular sections with heavier tool-joint areas. A suitable CNC pipe threading lathe needs adequate swing, chucking force, spindle torque, and support equipment for the tool-joint diameter. If the machine is sized only for standard pipe outside diameter, it may not handle the enlarged ends used in drilling assemblies.
Couplings and pup joints usually require shorter machining lengths but may involve larger diameters and more demanding internal threads. The machine should provide sufficient boring-bar clearance, internal tooling access, and repeatable positioning between multiple operations. For manufacturers producing several coupling sizes, quick program changes and tool presetting can reduce setup variation.
Pipeline components may include flanges, threaded connectors, nipples, and transition pieces. These components do not always use the same thread forms as OCTG products, so I confirm the control's threading cycles and the available tooling before purchase. NPT and BSP capability may be useful for industrial pipe work, but it should not be confused with full qualification for API-related connections.
I recommend sizing the machine from the largest and heaviest regular workpiece rather than the average pipe. A machine that handles a common 4-inch tube may still be unsuitable for a production line that occasionally processes 10-inch casing or a large coupling. The following specifications should appear in the quotation and technical acceptance document.
| Specification | Why it matters | Buyer verification point |
|---|---|---|
| Spindle bore | Determines the largest pipe or bar that can pass through the spindle | Confirm usable bore, not only nominal bore |
| Maximum turning diameter | Defines the largest external diameter above the bed or carriage | Check diameter over bed and over cross slide |
| Machining length | Determines whether the pipe end can be completed in one setup | Compare usable travel with actual thread length |
| Spindle speed and torque | Affects cutting stability, material removal, and large-diameter threading | Request speed range and torque curve |
| Motor power | Supports heavy cuts and larger tools | Confirm continuous and peak ratings |
| Chuck configuration | Controls workholding force and concentricity | Compare hydraulic, manual, three-jaw, four-jaw, or dual-chuck options |
| Thread-pitch range | Determines compatible thread families and production flexibility | Request metric and inch ranges separately |
| Support arrangement | Reduces vibration and deflection on long workpieces | Confirm steady rest, rear chuck, roller support, or follow rest |
| CNC control | Determines programming, synchronization, diagnostics, and data handling | Specify control brand, threading functions, and backup method |
For large-bore work, rigidity is as important as motor power. A flexible bed, weak carriage, or undersized cross slide can produce chatter even when the spindle motor appears sufficient. I therefore ask for machine weight, bed width, guideway design, carriage travel, spindle bearing arrangement, and a demonstration cut using material similar to the production pipe.
Dual-chuck arrangements can improve alignment and reduce movement during long-pipe machining. A front chuck may hold the pipe while a rear chuck or support device controls runout farther along the workpiece. This is especially useful for long tubing, drill-pipe sections, and thin-wall products that can deflect under cutting force.
The operator first loads the pipe, centers it, and secures it with a suitable chuck or dual-chuck arrangement. The CNC program then controls spindle rotation, carriage movement, tool position, cutting depth, thread pitch, taper, and retract sequence. The control synchronizes the feed axis with spindle rotation so that the tool follows the programmed thread geometry.
A typical cycle begins with facing and chamfering, followed by external or internal roughing. The machine then performs one or more threading passes, applies a thread relief or runout operation, and completes deburring or finishing work. The number of passes depends on material grade, thread size, tool geometry, required surface condition, and the machine's available torque.
For repeat production, the program can store tool offsets, work offsets, cutting parameters, and inspection points. This reduces manual calculation compared with a conventional pipe lathe. However, CNC control does not remove the need for correct workholding, tool setup, gauge calibration, chip control, coolant management, and operator training.
A CNC pipe thread cutting machine can produce different thread forms when the control, tooling, and mechanical capacity support them. Typical capabilities may include external and internal metric threads, inch threads, taper threads, NPT, BSP, and selected API-related profiles. The exact range depends on pitch capability, nose geometry, tooling, software cycles, and the pipe connection specification.
API thread machining requires more than entering a pitch value into the CNC control. The supplier and buyer must define the applicable product specification, thread profile, taper, crest and root form, standoff or reference dimensions, and inspection method. API-related work should be validated with calibrated gauges, thread measurement equipment, surface checks, and documented acceptance criteria.
I recommend a quality-validation workflow with five stages:
For high-pressure pipe connections, dimensional verification should be connected to the buyer's quality system and customer specification. A supplier should not claim API suitability only from a product label or catalog photograph. I ask for sample inspection reports, gauge details, repeatability data, and a factory acceptance test using representative pipe whenever the application involves critical connections.
A conventional pipe lathe can be practical for repair work, low-volume production, or operations where an experienced machinist adjusts each cut manually. Its initial acquisition cost may be lower, but the operator carries more responsibility for pitch calculation, tool positioning, repeatability, and process control. The result can vary more between shifts or operators unless the shop uses a disciplined setup procedure.
A CNC pipe lathe stores programs and coordinates spindle motion with axis feed. This makes it more suitable for repeated casing, tubing, and coupling orders with defined thread dimensions. The financial benefit depends on production volume, changeover frequency, labor rates, rejection costs, and the value of shorter cycle times rather than on the machine label alone.
A general CNC turning center may offer higher spindle speed and compact automation for smaller parts. It is often a good choice for shafts, fittings, and components that fit within a smaller spindle bore. However, many standard turning centers do not provide the bore, chuck capacity, bed length, torque, or pipe-support arrangement required for large oilfield tubulars.
An oil-country lathe is usually configured around long hollow workpieces and thread operations. It may sacrifice some compactness or high-speed turning performance in exchange for through-bore capacity, large workholding, and heavy-cutting stability. I select a general CNC turning center only when the pipe diameter, length, weight, and connection geometry remain within its verified limits.
I use an application-sizing worksheet before comparing brands or prices. The worksheet should list pipe outside diameter, inside diameter, wall thickness, total length, threaded length, material grade, maximum weight, thread type, production quantity, and required inspection method. These values provide a more reliable basis for selection than a general statement such as “large capacity.”
| Production requirement | Machine feature to prioritize |
|---|---|
| Large casing or tubing | Spindle bore, chuck diameter, motor torque, and bed rigidity |
| Long drill-pipe sections | Dual chucks, steady rests, roller supports, and usable machining length |
| Frequent coupling production | Fast chucking, tool presetting, stored programs, and boring capacity |
| API-related connections | Synchronized threading, precise control, gauges, inspection records, and acceptance testing |
| Mixed metric and inch work | Broad pitch range and clearly specified threading cycles |
| Small oilfield manufacturer | Practical automation, accessible maintenance, training, and manageable installation cost |
| High-volume production | Chip evacuation, coolant capacity, tool monitoring, repeatable loading, and spare-parts planning |
The supplier should also explain installation requirements. These may include foundation design, electrical supply, compressed air, hydraulic oil, coolant, lifting equipment, environmental conditions, and operator training. I request a layout drawing, machine weight, shipping dimensions, commissioning plan, warranty scope, response time, and recommended spare-parts list before placing an order.
GSK identifies itself as Shandong GSK CNC Equipment Co., Ltd., a CNC machine manufacturer based in Tengzhou, Shandong, China. Its published company information states more than 30 years of machine-tool experience, a 100,000-square-meter operating area, more than 200 employees, annual output of 2,500 sets, and exports to more than 150 countries and regions.
The company lists CNC machining centers, CNC lathes, milling machines, and related equipment in its product range. It also states that it can provide ISO, CE, BV, TUV, SGS, EAC, ERP, and WIPO certificates, along with complete QC testing and an 18-month warranty. For a pipe-threading purchase, I would still request the certificate applicable to the exact machine, because company-level statements do not replace model-specific documentation.
| Supplier or machine category | Main advantage | Main verification requirement |
|---|---|---|
| Premium international machine brand | Established controls, service network, and documented options | Confirm lead time, local service cost, and total installed price |
| Factory-direct Chinese supplier such as GSK | Potentially competitive purchase price and customization discussion | Verify model-specific specifications, FAT results, warranty, and spare-parts support |
| Conventional pipe lathe | Lower process complexity and useful manual flexibility | Compare labor, repeatability, inspection, and production-rate costs |
| General-purpose CNC lathe | Flexible for smaller components and mixed turning work | Confirm bore, chuck, torque, length, and thread-cycle limits |
Automation can include hydraulic chucking, automatic lubrication, chip conveyors, bar or pipe loaders, steady-rest positioning, tool presetting, probing, and workpiece measurement. I do not assume that every automation option improves the process; it must reduce loading time, setup variation, or operator exposure without creating difficult maintenance tasks.
A maintenance plan should cover daily chip and coolant removal, lubrication checks, hydraulic pressure inspection, chuck cleaning, guideway protection, toolholder inspection, and alarm review. Weekly or monthly checks may include spindle runout, chuck jaw condition, steady-rest alignment, coolant concentration, electrical cabinet filters, and backup of CNC parameters. The exact interval should follow the machine manual and the operating environment.
Reliability should be evaluated through evidence rather than adjectives. I ask about spindle bearing life, control replacement availability, common alarms, mean repair response, remote diagnostic capability, local technician coverage, and stocked wear parts. A production line can lose more money from a two-day control or chuck failure than from a modest difference in initial machine price.
A realistic quotation should separate the base machine from chucking, tooling, gauges, steady rests, chip conveyors, coolant systems, installation, training, packaging, freight, import charges, and commissioning. Indicative market planning bands may range from approximately $40,000 to $90,000 for smaller or more basic factory-direct configurations, $90,000 to $180,000 for larger automated machines, and above $180,000 for premium branded systems with extensive automation and service coverage. These are budgeting ranges, not supplier quotations.
I calculate ownership cost using the following structure:
Five-year cost = purchase price + installation + tooling + gauges + energy + maintenance + labor + downtime + rejected parts − resale value.
For example, if a machine reduces a threaded-pipe cycle from 18 minutes to 12 minutes across 1,600 parts per year, it saves 160 machining hours annually before accounting for setup and inspection. If one rejected connection costs $180 in material, labor, and rework, preventing 40 rejects saves $7,200 per year. These figures must be replaced with the buyer's actual production data before approving an investment.
Before requesting a final CNC pipe threading lathe machine quotation, I confirm the following items:
A CNC Pipe Threading Lathe Machine for Oil and Gas Industry Applications should be selected from measured workpiece requirements, not from nominal machine size or a general product description. I begin with spindle bore, chuck capacity, turning diameter, machining length, torque, support arrangement, and thread-pitch range, then verify whether the control and tooling can produce the required internal and external profiles.
For OCTG pipe threading, API thread machining, casing, tubing, drill pipe, and coupling work, the purchase decision must also include gauges, inspection records, acceptance testing, automation, maintenance, technical support, and installation planning. GSK's stated production scale, export coverage, certificates, QC testing, and 18-month warranty provide useful supplier information, but I would still request model-specific specifications and a representative factory test.
The next practical step is to prepare a dimensional workpiece list and send it to each shortlisted supplier. Ask for a complete quotation, five-year cost estimate, inspection plan, and acceptance criteria so that machine capability can be compared with documented evidence rather than marketing claims.
Previous: None
Next: BT40 vs. BT50 Spindle: How to Choose the Right Vertical Machining Center
Navigation
Tel.: +86 632 5083 879
Mob.: +86 151 6326 5369
Wechat: +86 151 6326 5369
E-mail: info@gskequipment.com
WhatsApp: +86 151 6326 5369